If you’ve ever needed a component that fits perfectly, handles extreme stress, and stands the test of time—whether it’s for heavy machinery, industrial pumps, or construction equipment—you know that boring welding isn’t just a service. It’s the backbone of reliability. As someone who’s run a boring welding supplier for 12 years, I’ve seen firsthand how a rushed, unregulated process can turn a simple repair into a costly failure (ask me about the 2018 pump shaft disaster that set a local plant back 10 days, if you want a war story). The difference between a job that lasts 6 months and one that lasts a decade comes down to one non-negotiable: a rigorous quality control (QC) process that doesn’t just check boxes at the end—it’s woven into every single step. Let’s break down exactly what that looks like from a supplier who’s lived and breathed this work. Boring Welding
First, before we even touch a welding torch or a boring bar, there’s a pre-process QC stage that most competitors skip. I call it the “start with the part, not the project” check. Too often, vendors take a customer’s broken component, grind off the old weld, and jump straight to machining or welding without verifying the core of the part itself. That’s how you end up repairing a part that’s already cracked at the base metal, or has hidden impurities that will cause failure down the line. Our team’s first step, every single time, is a full audit of the raw part or the new component we’re working with.
For example, last quarter we had a customer bring in a 12-inch diameter shaft for a heavy-duty mixer—they’d had it welded by a shop that skipped pre-process checks, and the shaft broke mid-repair. Our first move wasn’t to grab the boring bar; we ran a magnetic particle inspection (MPI) on the entire shaft. MPI uses a magnetic field and iron particles to reveal tiny surface or subsurface cracks that are invisible to the naked eye. Turns out, the shaft had a 2mm-long crack at the bearing seat the customer hadn’t mentioned. If we’d welded over that, it would have failed within a month, not 6 months. We flagged it, had the customer replace the shaft’s end, and then we moved forward. That’s not overcaution—that’s QC as a safety net, not a chore.
We also verify all incoming materials and consumables during this pre-process stage. Welding rods, electrodes, and even the boring bar inserts are only as good as their specifications. Last year, a new supplier sent us a batch of E7018 welding rods that were labeled correctly but tested 10% lower in tensile strength than we required. Instead of using them (and risking a bad weld), we sent them back, even though it delayed two small jobs. A week later, that supplier issued a recall for that exact batch—turns out, they’d mixed in lower-grade rods to cut costs. If we’d used those, we’d have been on the hook for every warranty claim, not to mention our reputation. So pre-process QC includes: material certification checks, MPI/ultrasonic testing (UT) of the base part, equipment calibration (our boring lathes are checked for alignment every morning, before the first part), and a written approval from a QC lead that the project is ready to proceed.
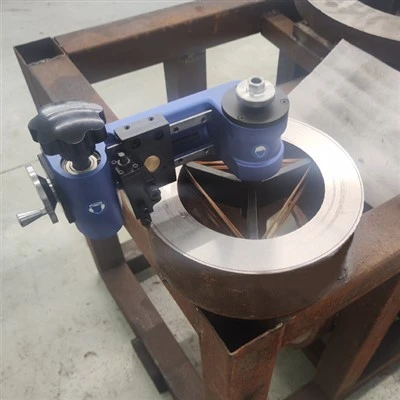
Next comes the core work: the boring and welding operations themselves, where QC is baked into each step, not just a final check. Boring welding is two parts: first, you machine (boring) a precise cavity or seat into the part to fit a new component or repair the worn area, then you weld that part in place, making sure the joint is strong and perfectly aligned. One small mistake here—even a 0.1mm misalignment or a weld with hidden porosity—can render the entire part useless.
For boring, we use coordinate measuring machines (CMMs) for critical parts, but for larger components that can’t fit on a CMM, we use dial indicators and bore gauges that are calibrated daily. Let’s take a worn pump liner, a common repair job: the customer’s liner has a 2mm wear groove that’s throwing off pump performance. Our boring machinist’s first step is to set the part in a hydraulic fixture that locks it in place, then we take three separate diameter measurements at 0°, 90°, and 180° to ensure the axis is perfectly parallel to the machine’s spindle. If the fixture is off by even 0.05mm, the boring cut will be uneven, and the liner won’t seat properly. We document every measurement—no exceptions. Every machinist has a QC checklist they sign after each boring pass, and that checklist is filed with the part’s job history.
Then comes welding, the stage where most QC shortcuts happen because welding is often seen as a “skill-based” job, something that doesn’t need strict checks. That’s a myth. We only use AWS (American Welding Society) certified welders, and even then, every weld we do undergoes immediate post-weld inspection. First, we do a visual inspection: no spatter that’s not ground off, no undercut (a shallow groove along the weld edge that weakens the joint), no porosity (tiny air pockets that form when the welding rod is not applied correctly). But visual checks only catch surface issues—for internal flaws, we use UT, which sends sound waves through the weld to detect cracks or porosity that are hidden. Last year, we had a welder who was rushing a small bracket weld for a forklift part. The visual check looked fine, but UT revealed a 1mm crack in the root of the weld. We re-did the weld, not because the welder was bad, but because rushing leads to mistakes. That’s why we mandate a 15-minute “cool down” between weld passes for high-stress applications—heat buildup causes distortion, which is another failure point. We don’t let anyone skip that.
Another key part of in-process QC is distortion control. When you weld a part, heat makes it warp, which ruins alignment. For long shafts, we use pre-weld fixtures that apply mild tension to the shaft as we weld, so when it cools, it stays straight. For larger components, we use intermittent welding (short, spaced weld passes) instead of a single long weld, which reduces heat buildup. We measure part alignment before, during, and after each weld pass. If a shaft warps more than 0.1mm, we adjust the fixture and re-weld that section. It’s extra work, but it’s the work that separates us from the shops that see 10% of their parts come back for rework.
Once the boring and welding is done, we move to post-process QC—the final gate before a part leaves our facility. This isn’t a quick once-over; it’s a battery of tests tailored to the part’s use case. For precision components like turbine shafts, we use CMMs to verify dimensional accuracy down to 0.01mm. For high-stress parts like construction equipment boom pins, we do a magnetic particle inspection again to catch any cracks that formed during welding or cooling. We also perform pressure testing on parts that handle fluids—like hydraulic cylinders or pump liners. We pressurize the part to 150% of its working pressure and hold it for 10 minutes, checking for leaks or deformations. That pressure test caught a bad weld on a hydraulic cylinder for a forestry company last year—we re-welded it, and that cylinder has now done 3 years of heavy duty without a problem.
We also document every single step of the QC process for every part. Each job has a digital file that includes pre-process material certifications, boring measurement logs, weld inspection reports, non-destructive testing (NDT) results, and final dimensional checks. When a customer gets their part, they get a copy of that file. It’s not just a nice touch—it’s proof that we didn’t cut corners. A few months ago, a customer said to me, “I don’t need a report, just send the part.” I told him no—he needed to know that the part he was putting in his $2 million production line was built to spec, with verified checks at every step. That report has become our biggest selling point: customers don’t just trust the part, they trust the process that made it.
I’ve heard some competitors say that our QC process is too slow, too expensive. But I’ll take 2 extra days of checks over a $50,000 warranty claim because a part failed. Last year, our rework rate was 0.8%—that means only 8 out of 1,000 parts we made needed fixes, and those were all due to customer error, not our process. Most shops have a rework rate of 5-10%, and that eats into profits way more than a little extra QC time.
At the end of the day, boring welding is about reliability. Whether you need a repair that gets your production line back up in 2 days, or a custom component for a new project, you need to know that the part will work when you turn it on, and keep working for years. Our QC process isn’t a set of rules we follow because someone told us to—it’s how we treat every part as if it were our own. We’ve been in this business long enough to know that a broken part isn’t just a lost sale; it’s a customer who can’t meet their own deadlines, and that’s something we never want to be responsible for.

If you need a boring welding supplier that doesn’t just do the job, but proves every step of the process, we’re here to help. We work with small local shops and large national corporations, and we tailor our QC to your needs—whether you need standard repairs or custom precision parts. Reach out to our team to discuss your project, get a transparent quote, and see how our rigorous quality control can give you the reliability you need.
Keyway Milling References
AWS D1.1/D1.1M: Structural Welding Code – Steel. American Welding Society, 2020.
Lancaster, J.F. Metallurgy of Welding and Weldability. Woodhead Publishing, 2017.
ASME B46.1: Surface Texture (Surface Roughness, Waviness, and Lay). American Society of Mechanical Engineers, 2022.
Shangqiu JDA Machinery Technology Co., Ltd.
With abundant experience, we are one of the most professional boring welding manufacturers and suppliers in China. We warmly welcome you to buy cheap boring welding for sale here from our factory. Quality products and reasonable price are available.
Address: No. 55 Pingyuan Middle Road, Liangyuan District, Shangqiu, Henan, China
E-mail: sales@jdamachines.com
WebSite: https://www.jdamachines.com/
